Start with a clean, flat sorting area
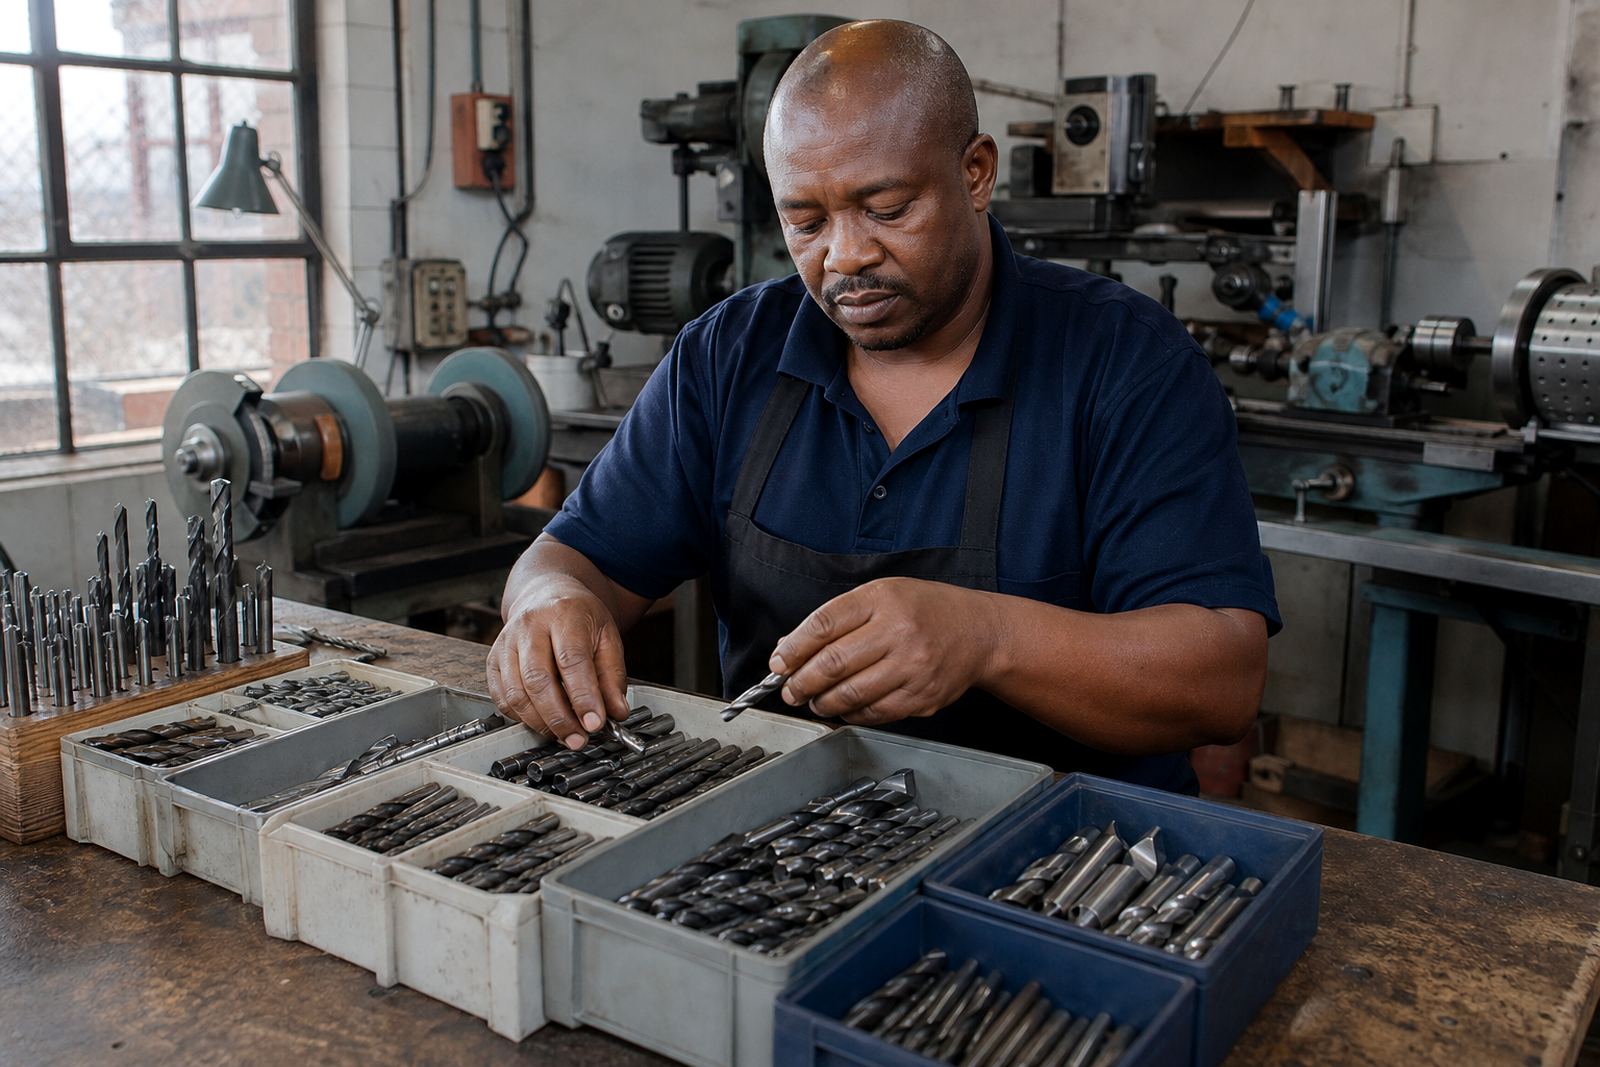
Lay the drills out on a clean bench, tray or floor sheet where you can see every piece. Good light matters, especially when you are checking wear, burn marks and chipped tips on small diameters like 1 mm to 6 mm.
If the batch has come from a site box, workshop drawer or van storage crate, wipe off cutting fluid, dust and swarf first. This helps you spot twisted flutes, split points and overheat discolouration, and it keeps grit out of the regrinding machine. In humid coastal areas around Durban and Pinetown, a quick wipe also helps stop light surface rust from spreading before the tools are checked.
Separate drill types before you measure anything
Mixing drill types slows the whole job down. Sort by body shape and cutting style first, then group by size. Standard twist drills should stay apart from masonry drills, stepped drills and any specialist bit that is not meant for the same process.
- Twist drills for metal and general workshop use
- Masonry drills with carbide tips
- Step drills and special profile bits
- Left hand or reverse cut drills
- Long series drills that need careful handling
If the batch includes a few odd pieces, put them in a separate tray and mark them for review. That simple step avoids the wrong angle being ground onto a tool that should not be treated like the rest.
Group by diameter and length for faster set-up
Once the drill types are separated, group them by diameter. Small batches can be sorted by eye, but for mixed work it helps to use a vernier caliper or a drill gauge. Put together all drills with the same size or as close as possible, then separate short drills from long ones.
Length matters because longer drills need different handling and sometimes extra support during sharpening. A pile of 3 mm drills should not be mixed with 3 mm long-series drills, even if they look similar at first glance. It saves rechecking later and makes batch tagging easier when we collect from Pinetown, Durban, Westville or Hillcrest.
- Measure the shank first, then the cutting diameter
- Keep fractional or imperial sizes in their own groups
- Mark any drill that is undersized from wear
- Separate very short or snapped pieces for assessment
Sort by the fault that needs attention
Not every drill needs the same work. Some only need a clean sharpen, while others need chipped edge recovery, angle resetting or burn mark removal. Sort the batch by the main problem you can see, even if you are not sure about the full condition yet.
Look for these common issues: blunt points, one flute longer than the other, chipped corners, overheating, rounded lips, bent shanks and missing centre points. If a drill has several faults, place it in the most serious group so it gets checked properly. That keeps the batch from being rushed through the wrong process.
For workshop teams in Johannesburg, Pretoria and Cape Town, this step is useful when the same container has tools from different jobs. A bit of sorting now can prevent a lot of back tracking later.
Use simple batch tagging so nothing goes missing
After sorting, tag each group clearly. Batch tagging does not need to be complicated. A paper tag, label or marker note is enough if it shows the size range, drill type, fault and quantity. Keep the label with the tray or bag from start to finish.
- Batch name or client reference
- Type of drill
- Size range
- Main fault or service needed
- Quantity in the group
If the batch is leaving your site by courier, make sure the labels stay readable after packing. Use a sealed bag or box so the drills do not rattle loose in transit. One mixed lot with no tag can waste a full round of checking, especially when there are several identical sizes in the same consignment.
Check safety and condition before courier collection
Before collection, do a final walk-through. Remove loose packaging tape, broken drill cases and any bits of debris that could cut into the parcel. Make sure sharp ends are wrapped or secured, and keep carbide tipped pieces separate from standard steel drills where possible.
This is also the time to pull out anything unsafe to process, such as severely bent drills, cracked tips or bits with damaged shanks. Those items may need extra assessment before sharpening. If the batch is ready for courier collection, place the box in a dry spot away from moisture and direct sun, then confirm the parcel details on the enquiry form so the pickup can be arranged without delays.
For clients handling regular workshop maintenance, a simple pre-sort routine helps every time power interruptions, busy production days or load-shedding interruptions interrupt normal work. Less confusion at the collection point means less waiting later and a cleaner handover overall.